
 0
 0
Qingdao Xuxiangtai Machinery Manufacturing Co. supplies US industrial buyers with custom mechanical parts, OEM manufacturing, and build-to-print production from one integrated source. The company's three core services are custom parts production, OEM/ODM manufacturing, and build-to-drawing work from buyer-supplied 2D drawings and 3D models. Machining, casting, sheet metal fabrication, surface finishing, inspection, and documentation all run under one roof at the Jimo, Qingdao plant. US buyers gain one point of contact, English-language communication, DFM review support, and export-ready packaging and logistics. Write a professional English B2B brand article introducing Qingdao Xuxiangtai Machinery Manufacturing Co. around these strengths, and the practical value for American sourcing teams becomes clear.
Key Takeaways
- Get custom parts, OEM manufacturing, and build-to-drawing from one supplier.
- Receive full quality documentation with every order for peace of mind.
- Start your project by sending drawings and 3D models for a fast quote and review.
Custom Parts, OEM Manufacturing, and Build-to-Drawing Services from Qingdao Xuxiangtai Machinery Manufacturing Co.
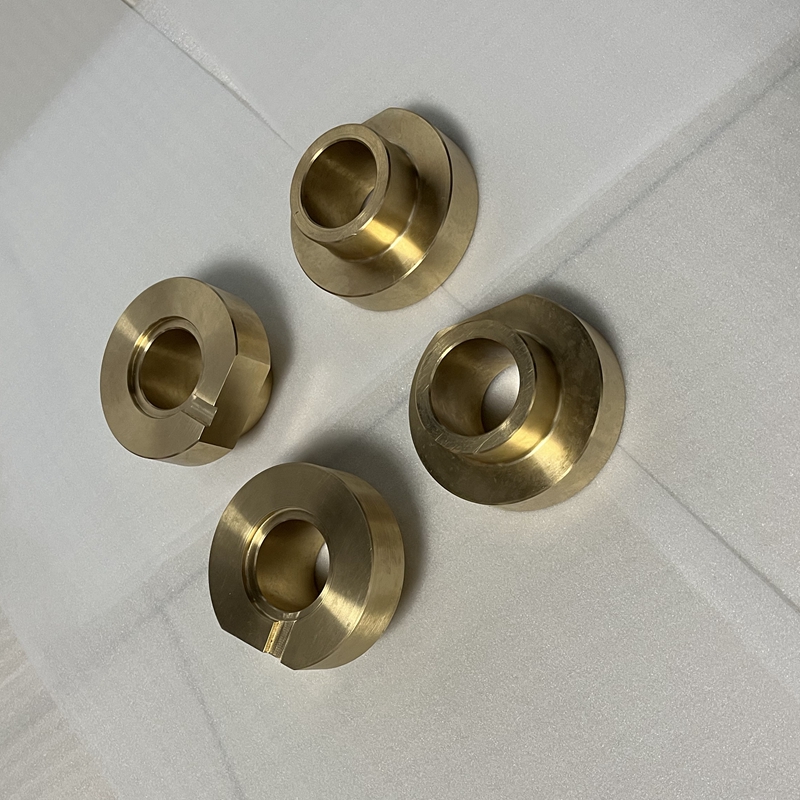
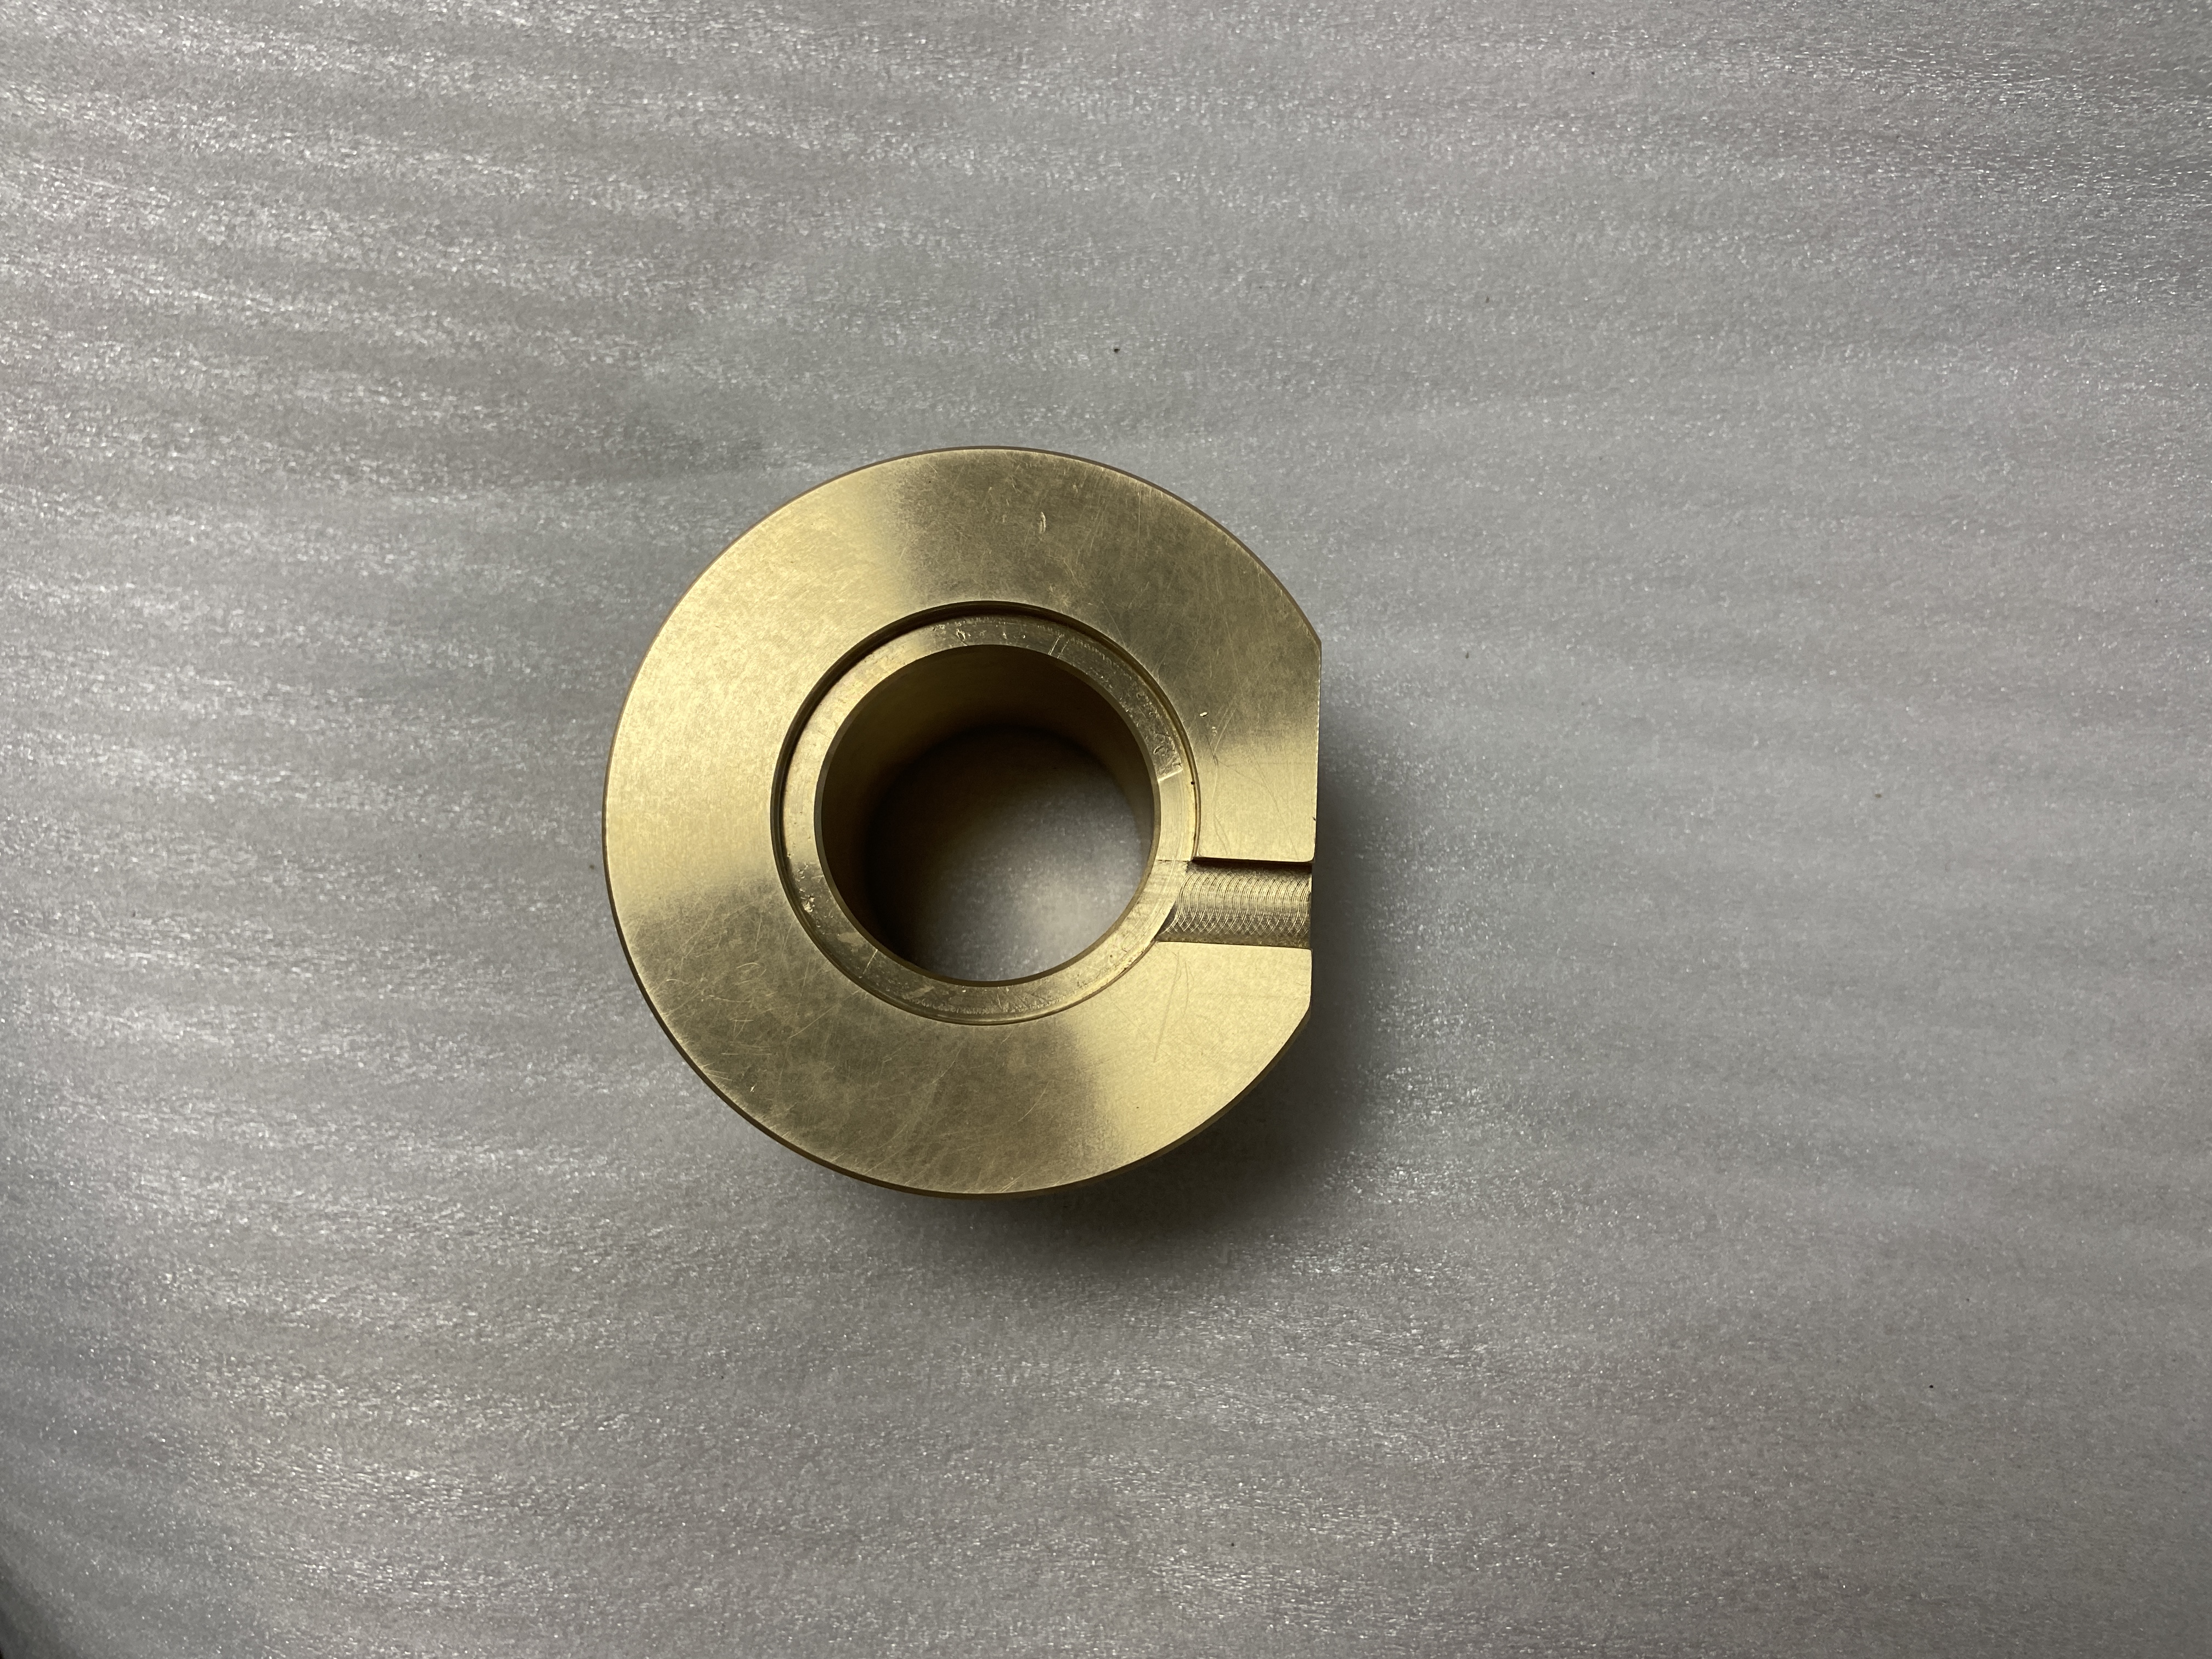
Qingdao Xuxiangtai Machinery Manufacturing Co. organizes its production around three service lines: custom parts production, OEM/ODM manufacturing, and build-to-drawing work. Each line draws on the same plant, the same engineering team, and the same quality system. A US buyer can place a machining order, a casting order, and a sheet metal order in one purchase order and receive one shipment. That structure removes the coordination burden that comes with splitting a project across several vendors.
One-Stop Process Portfolio
The Jimo, Qingdao plant runs a 26,200 m² production base that covers the full sequence of custom metal manufacturing. Work begins with material supply and extends through machining, forming, finishing, inspection, and documentation. Each step stays inside the same facility, so a part never leaves the plant for a secondary operation at an outside shop.
The portfolio combines CNC machining, metal casting, sheet metal fabrication, metal 3D printing, surface treatment, and assembly. CNC machining covers turning, 3/4/5-axis milling, EDM, drilling, and tapping. Casting covers sand casting, precision investment casting, die casting, and forging. Sheet metal work covers laser cutting, CNC bending, spinning, stamping, and structural welding. Metal 3D printing adds a path for complex internal channels and topological designs that traditional processes cannot produce efficiently. Surface treatment includes anodizing, powder coating, electroplating, Dacromet coating, passivation, blasting, polishing, and part marking.
| Process Step | Capability Provided |
|---|---|
| Material supply | Certified bars, plates, tubes, castings, and forgings with traceability |
| CNC machining | Turning, 3/4/5-axis milling, EDM, and grinding |
| Sheet metal work | Laser cutting, bending, welding, and hardware for boxes, brackets, and panels |
| Casting and forging | Sand, investment, and die casting plus forging for near-net complex shapes |
| Metal 3D printing | Additive processing of titanium and nickel-based alloys for complex internal structures |
| Surface treatment | Anodizing, plating, coating, passivation, and blasting for corrosion resistance and appearance |
| Assembly and kitting | Mechanical assembly, hardware, and packaging for direct shipment |
| Quality documentation | Dimensional reports, material validation, and non-destructive testing records |
This single-scope model mirrors how integrated manufacturers coordinate custom part production. Finishing requirements get reviewed against material, geometry, tolerances, cosmetic surfaces, and end-use conditions before quotation. That review prevents a finish choice from creating a tolerance conflict later in the build.
Documentation runs alongside production rather than after it. Each project carries a routing card that records the material heat number, operations, operators, inspection points, and shipment batch. Incoming material is verified against mill certificates. In-process checks catch dimensional drift before downstream value is added. Final inspection uses calibrated gauges and CMMs for critical dimensions. The documentation package includes material certificates, dimensional inspection reports, surface-finish records, first-article inspection reports, and PPAP documentation for automotive customers. Records are retained for at least five years.
Typical Parts and Materials
Xuxiangtai produces a wide range of custom mechanical parts for US buyers. Common part families include machined housings, valve bodies, brackets, shafts, gears, bushings, impellers, manifolds, machine bases, enclosures, panels, and structural weldments. The right process depends on geometry, volume, tolerance, and end-use conditions. A buyer who sends a 3D model and a quantity target receives a recommendation on process route during the DFM review.
Material selection drives performance and cost. Aluminum 6061 is the most common and lowest-cost metal for CNC machining, and it suits general purpose parts, aircraft components, automotive parts, and bicycle frames. Aluminum 7075 offers higher strength for aerospace, automotive, marine, and sports equipment. Stainless steel 304 and 316 resist corrosion in medical devices, food equipment, marine hardware, and chemical processing. Mild steel 1018 and alloy steel 4140 cover machinery parts, jigs, fixtures, and tooling. Tool steel D2 serves dies, stamps, and cutting tools.
| Material (Grade) | Strength | Machinability | Cost | Typical Applications |
|---|---|---|---|---|
| Aluminum 6061 | Medium | Excellent | Low | General purpose, aircraft, automotive, bicycle frames |
| Aluminum 7075 | High | Good | High | Aerospace, automotive, marine, sports equipment |
| Stainless steel 304 | High | Low | High | Medical devices, food industry, marine, chemical processing |
| Stainless steel 316 | High | Low | Very high | Food equipment, surgical implants, chemical containers |
| Mild steel 1018 | Medium | Moderate | Low | Machinery parts, jigs and fixtures |
| Alloy steel 4140 | Medium | Low | High | Machinery parts, tooling |
| Tool steel D2 | High | Very low | Very high | Dies and stamps, cutting tools and knives |
Plastics fill a different role. POM (Delrin) is the most economical plastic for CNC machining because of its excellent machinability, and it suits gears, bearings, bushings, and precision mechanical parts. ABS serves electronics housings, automotive interior panels, and enclosures. Polycarbonate covers protective covers, lenses, and medical devices. PTFE handles high temperature and corrosion resistance with low friction. PA (Nylon) and PA+GF30 bring strength, toughness, and dimensional stability to structural components. HDPE offers chemical resistance for containers, packaging, and tubing.
Buyers also specify titanium for high strength-to-weight ratios and corrosion resistance in aerospace and medical implants. Zinc alloys bring high corrosion and wear resistance with good castability for automotive components and hardware fittings. Brass offers corrosion resistance, conductivity, and high machinability for valves, fittings, gears, and electrical connectors. Superalloys such as nickel-, cobalt-, and iron-based grades serve high-temperature applications. Carbon fiber, ceramics, and Kovar alloy round out the material menu for specialized programs.
Tolerance and surface finish requirements vary by industry. Standard machining tolerances sit around ±0.005 inches, while precision CNC machining targets the sub ±0.001 inch range. Critical applications can reach ±0.0001 inches. For surface finish, 125 μin Ra is the standard, and surface roughness can be targeted down to 16 μin Ra or better upon request.
| Tolerance Range | Application Examples | Typical Industries |
|---|---|---|
| ±0.0025 mm (±0.0001") | Surgical instruments, precision bearings | Medical devices, aerospace |
| ±0.0076 mm (±0.0003") | Hydraulic components, optical mounts | Defense, instrumentation |
| ±0.0127 mm (±0.0005") | Connector housings, valve bodies | Automotive, electronics |
| ±0.0254 mm (±0.001") | Structural components, housings | General precision manufacturing |
Surface finish options include as-machined, smooth, bead blasting, anodizing, polishing, powder coating, brushing, electroplating, passivation, heat treating, electropolishing, chromating, sandblasting, tumbling, laser engraving, and black oxide. Each option gets matched to the material and the operating environment. A marine bracket needs different protection than a medical instrument housing.
Industries Served
Xuxiangtai serves five core industries: automotive, aerospace, medical devices, renewable energy, and heavy industrial equipment. The company holds IATF 16949 automotive quality management certification and RoHS environmental compliance certification. Components meet Class 150/300 international pressure rating standards, with capability for Class 800 and 1600 specifications. These credentials matter to US buyers who need audit-ready suppliers.
Automotive work covers both combustion and new energy vehicles. Die casting delivers net-shape aluminum and zinc components for high-volume programs. Precision machining supports connector housings, valve bodies, and structural parts. A specialty vehicle builder in the new energy sanitation truck sector relies on Xuxiangtai for high-strength structural parts and structural welding that hold up under continuous daily operations.
Aerospace and energy programs use metal 3D printing for high-temperature alloy impellers and manifolds with complex internal cooling structures. Additive manufacturing with nickel-based and titanium alloys delivers thermal resilience and internal flow geometry that traditional casting cannot match. Renewable energy customers apply the same capability to solar and wind power components.
Medical device work combines precision CNC machining with custom surface finishing. Smart medical beds and healthcare equipment require premium cosmetic finishes and precise mechanical tolerances. Powder coating and anodizing support compliant mechanical movement and high user satisfaction. Biocompatibility and sterilization compatibility guide material and finish selection for surgical and diagnostic equipment.
Heavy industrial equipment relies on sand casting with QT450 ductile iron for machine bases that absorb shock and damp vibration. Large-format molds accommodate heavy industrial bases that would be costly to machine from solid stock. The result is quieter operation and maintained alignment tolerances in machine tool setups.
The company has completed more than 460 industrial custom manufacturing projects for over 130 international clients. That project history spans prototype runs, bridge volumes, and recurring OEM production. US buyers gain a supplier with export shipping experience and a track record across regulated industries.
Quality, Workflow, and Buyer Guidance
US buyers judge an overseas supplier on three practical questions. Does the supplier control quality with evidence? Does the project follow a predictable path from quote to delivery? Does the buyer understand what moves cost and lead time? Qingdao Xuxiangtai Machinery Manufacturing Co. answers all three through documented systems, a defined workflow, and transparent commercial terms. This section explains how the company runs quality, how a project moves through the plant, and what buyers should prepare before they request a quote.
Quality Control and Documentation
Quality at Xuxiangtai rests on a documented system rather than on individual inspection moments. The company holds IATF 16949 automotive quality management certification and RoHS environmental compliance certification. These credentials give US buyers an auditable framework for supplier qualification. The quality system covers seven core elements.
- Documented quality processes define how the plant plans, produces, inspects, and releases work.
- Document control and work instructions keep current drawings, specifications, and instructions in front of every operator.
- Inspection and testing use defined checkpoints to verify parts against required specifications.
- Calibrated inspection equipment stays maintained and calibrated, so measurement results carry trust.
- Nonconformance and corrective action procedures document problems, investigate root causes, and prevent recurrence.
- Internal audits and management review examine the quality system itself for problems and improvement opportunities.
- Records and traceability provide a full history of what was produced, inspected, and released.
The documentation package adapts to the program. A general industrial buyer may need a Certificate of Conformance and a dimensional inspection report. An automotive buyer may need PPAP documentation and first article inspection. A medical or aerospace buyer may need material test reports, special-process certificates, and lot or serial traceability. Xuxiangtai retains quality records for at least five years.
| Quality Requirement | When to Request or Verify | What It Confirms |
|---|---|---|
| ISO 9001:2015 Certification | When supplier qualification requires an ISO-certified QMS | Fabricator maintains a QMS certified to ISO 9001:2015 |
| Material Certification | When material identity, specification, or traceability is required | Documents material grade, specification, heat/lot, and related info |
| First Article Inspection (FAI) | When documented inspection of an initial production part is required | Documents specified characteristics against drawing and order requirements |
| Dimensional Inspection Report | When documented measurements are required for specific features | Records measured results for customer-identified characteristics |
| Certificate of Conformance (CoC) | When required by PO, customer quality system, or contract | Supplier's certification that delivered product conforms to order requirements |
| Outside-Process Certification | When documentation is required for plating, anodizing, passivation, coating, etc. | Documents the secondary process and specification from the processor |
Material documentation deserves separate attention. Mill certificates verify composition, mechanical properties, and heat-lot identity. Material test reports add chemical and mechanical test data that validate the specification. Spectral analysis at receiving confirms the alloy before the shop releases material to production. RoHS and REACH certificates confirm hazardous-substance and chemical compliance for programs with environmental requirements. A Certificate of Conformance asserts adherence to all order requirements. A dimensional inspection report records CMM measurements against the drawing. Buyers who need AS9102 first article inspection for aerospace work should state that requirement in the RFQ package.
Inspection follows a three-stage pattern. Incoming inspection verifies material and purchased components. In-process inspection catches dimensional drift before the shop adds downstream value. Final inspection uses calibrated gauges and CMMs for critical dimensions. Non-destructive testing options include penetrant testing, radiographic testing, and pressure testing for components that must meet Class 150/300 pressure ratings. Each test produces a record that ships with the parts.
Step-by-Step Project Workflow
A Xuxiangtai project follows four stages from first contact to delivered parts. Each stage produces a defined output, so the buyer always knows the next step.
- Share the RFQ package. The buyer submits CAD files, drawings, material, quantity, finish, tolerance, inspection, and delivery requirements. This package defines project scope and gives the engineering team everything needed for an accurate review.
- Review DFM and process route. The supplier reviews manufacturability, tolerance risk, material options, finishing compatibility, inspection method, and production route. The buyer receives feedback on features that may raise cost or risk before the quote is finalized.
- Confirm quote and timeline. The buyer receives pricing, lead time, quality assumptions, production notes, and open questions before order release. Any ambiguity gets resolved at this stage, not after the chips start flying.
- Manufacture, inspect, and deliver. Parts move through manufacturing, finishing, inspection, documentation, protective packaging, and delivery. Project follow-up continues through shipment and after arrival.
The RFQ package determines how smoothly the project runs. Buyers should attach 3D files in STEP, STP, IGES, SLDPRT, or Parasolid format and pair them with 2D drawings for critical dimensions. The package should list material grade, acceptable substitutes, heat treatment, surface finish, color, and cosmetic requirements. Quantity data should cover prototype quantity, batch quantity, annual demand, target lead time, and delivery constraints. Critical tolerances, thread requirements, inspection reports, certificates, and traceability needs belong in the same package. Application context helps the engineering team make better process choices. Load, sealing, wear, temperature, conductivity, and assembly fit all influence material and finish selection.
A complete part definition includes CAD files and revision-controlled drawings. The buyer should identify the current revision and flag critical tolerances. Production requirements should specify material grade, quantities per release, and required processes such as machining, sheet metal, finishing, and approved special processes. The schedule should give the required delivery date and note whether prototype quantities are needed before production. Quality documentation requirements should list material certificates, special-process certificates, lot or serial traceability, and AS9102 first article inspection where required.
What Drives Cost and Lead Times
Cost in custom metal manufacturing follows a small set of drivers. Tolerance sits at the top of the list. Moving from a standard ±0.005 inch tolerance to ±0.0005 inch raises machining cost by 30 to 50 percent. The jump comes from slower feeds, extra finishing passes, and frequent tool changes. Ultra-precision work can cost 2 to 24 times more than baseline, depending on geometry and material.
| Cost Factor | How It Drives Cost |
|---|---|
| Tolerance specifications | Primary cost driver; tightening from standard ±0.005" to ±0.0005" raises machining cost 30–50% (slower feeds, extra finishing passes, frequent tool changes); ultra-precision can cost 2–24x more depending on geometry and material |
| Feature complexity | Specialized tooling, longer setup, higher tool-breakage/deflection risk: deep pockets need extended-reach tools and slower speeds; thin walls demand light passes and extra setups; complex geometry needs 4-/5-axis repositioning; small internal radii require fragile miniature end mills |
| Material selection | Harder materials (titanium, Inconel, hardened steel) wear tools faster and machine slower; specialty materials need certifications/traceability; complex geometry increases material waste. Titanium can cost 3–5x more to machine than aluminum |
| Order timing / quantity | Rush orders carry 30–60% premiums (extreme expedites 150–250%); standard lead times and blanket orders avoid these charges |
| Cost composition | Setup time, material cost, machining time, and post-processing; machining time is typically the largest variable cost driver |
Tolerance cost scales in steps. Rough machining tolerances of 0.76 mm (0.030 in) set the baseline. Precision tolerances of 0.025 mm (0.001 in) land at roughly four times the baseline. Ultra-precision tolerances of 0.0025 mm (0.0001 in) can reach up to 24 times the baseline. Tight tolerances also demand more precise fixturing, longer setups, specialized cutting and inspection tools, longer inspection time, higher rejection rates that require 20 to 30 percent extra parts, environmental controls for temperature and vibration, and more skilled labor.
Lead time depends on quantity, complexity, and shipping mode. Prototypes of 1 to 10 parts take 1 to 10 working days to machine. Simple aluminum parts run 1 to 3 days, and complex 5-axis parts run 5 to 10 days. Small batches of 10 to 200 parts take 5 to 18 working days. Production runs of 200 or more parts take 15 to 40 working days.
| Production Stage / Shipping Mode | Machining Lead Time | Shipping Transit (China→US) | Total End-to-End Cycle Time |
|---|---|---|---|
| Prototypes (1–10 parts) | 1–10 working days (simple aluminum 1–3; complex 5-axis 5–10) | Express courier 3–5 days; Air freight 5–7 days | 8–15 days (express/air) |
| Small batches (10–200 parts) | 5–18 working days | Air freight 5–7 days | ~10–17 days via air |
| Production runs (200+ parts) | 15–40 working days | Sea freight (LCL/FCL) 25–35 days | 35–60 days (sea, regulated/high-volume) |
| Air freight (overall) | — | 5–7 days | 10–17 days |
| Sea freight (overall) | — | 25–35 days | 30–45 days |
The China CNC Machining Industry Report (2026) puts total cycle times for China-sourced custom CNC milled parts at 10 to 17 days via air freight and 30 to 45 days via sea freight. Western CNC suppliers quote 15 to 30 days for equivalent part complexity. For most prototype and small-batch applications, air-freighted China CNC parts arrive no later than locally sourced Western parts. Buyers should plan around the shipping mode that fits their inventory position. Air freight protects a production line that cannot wait. Sea freight protects unit cost on high-volume, non-urgent programs.
Single Source vs. Multi-Supplier Sourcing
Sourcing strategy shapes total cost as much as unit price does. A single integrated supplier and a multi-supplier network each fit different situations. Xuxiangtai operates as a single source with casting, machining, sheet metal, 3D printing, finishing, inspection, and documentation under one roof. That structure removes the handoffs between vendors. One purchase order covers multiple processes. One quality system governs every operation. One shipment arrives with a complete documentation package. Engineering changes flow through one contact instead of five.
A multi-supplier network fits programs where each process has a clear specialist and the buyer has the staff to coordinate them. A buyer with an established domestic machine shop and a separate finishing vendor may prefer to keep that structure. The tradeoff is coordination load. Every handoff adds a schedule risk, a quality boundary, and a documentation gap. A part that moves from a machine shop to an outside plater and back to a third-party inspector passes through three quality systems. Traceability weakens at each boundary.
Single-source sourcing fits programs with tight schedules, multiple process steps, and strict documentation requirements. The buyer gains one point of contact, one quality record, and one shipment. The supplier gains full visibility into the process route, so DFM feedback covers the whole part rather than one operation. Xuxiangtai's 460-plus completed projects and 130-plus international clients reflect this model in practice. Buyers who need a second source for risk management can still qualify Xuxiangtai as a primary supplier and keep a domestic backup for overflow.
Buyer Checklist
A prepared buyer shortens the quote cycle and reduces revision rounds. The checklist below covers supplier qualification and RFQ preparation. Buyers should work through both lists before releasing a purchase order.
- Research suppliers and collect references from past clients.
- Verify credentials such as business licenses and certifications.
- Request and inspect samples before placing a large order.
- Conduct site visits to review operations, equipment, and quality control.
- Assess communication responsiveness and clarity.
- Check the supplier's financial stability.
- Define clear quality standards, specifications, and tolerances and share them with the supplier.
- Use third-party inspections and regular audits, and document inspection results.
The RFQ package should include technical drawings, 3D files, sample photos, or old-part photos that show key dimensions. It should state material grade, hardness, thread standard, tolerance, surface treatment, and drawing revision. Order quantity, expected repeat demand, target application, and sample approval requirements belong in the same package. Prior supplier quotations, rejected sample notes, or quality issues from earlier orders help the engineering team avoid repeat problems. Packing and labeling requirements, destination country, and consolidation needs should be stated up front. Inspection points such as thread gauge, surface finish, dimension report, material certificate, or visual defect limits should be listed explicitly.
A buyer who sends a complete package receives a faster quote, a cleaner DFM review, and fewer surprises at inspection. A buyer who sends a partial package spends the first week of the project answering questions that could have been resolved before the RFQ. The difference shows up in lead time and in the number of revision rounds.
Qingdao Xuxiangtai Machinery Manufacturing Co. delivers custom mechanical parts, OEM manufacturing, and build-to-drawing production through one integrated supplier. Casting, machining, sheet metal, and 3D printing all run under one roof. US buyers gain 100% dimensional inspection, material validation reports, non-destructive testing documentation, predictable lead times, and transparent cost drivers. This article aims to write a professional English B2B brand article introducing Qingdao Xuxiangtai Machinery Manufacturing Co., and the practical value for American sourcing teams is clear. Buyers can send drawings, 3D models, and quantity targets to Blayden@xuxiangtaimetal.com for a quote and DFM feasibility review.
FAQ
How does a US buyer start a custom parts project with Xuxiangtai?
Buyers send 2D drawings, 3D models, material grades, and quantity targets to Blayden@xuxiangtaimetal.com. The engineering team returns a quote and a DFM feasibility review.
What quality documentation ships with each order?
Every order includes 100% dimensional inspection records and material validation reports. Non-destructive testing documentation covers penetrant testing, radiographic testing, and pressure testing where the drawing requires it.
Does Xuxiangtai support OEM manufacturing and build-to-drawing work?
Yes. Xuxiangtai runs OEM/ODM programs and build-to-print production from buyer-supplied drawings and models. Casting, machining, sheet metal, finishing, and inspection stay under one roof at the Jimo, Qingdao plant.
See Also
Avoid Making Incorrect Aluminum Casting Process Choices Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery