
 0
 0
Power generation operators evaluating safety valves for boiler applications face a narrow but critical set of requirements: certified overpressure protection, dependable automated relief action, and a manufacturing partner capable of supporting large-scale industrial projects without compromising quality consistency. XINTAI Valve Group Co., Ltd., a global manufacturer founded in 1998 and headquartered in Wenzhou, China, has built its business around addressing exactly this class of industrial flow control challenge across the oil and gas, chemical, power station, water treatment, metallurgy, and mechanical markets.
Why Boiler Safety Valves Demand Certified Reliability
Power stations and pressure vessel systems operate under conditions where excessive pressure build-up can endanger personnel and equipment. This is the core scenario pain point that safety valves are engineered to solve. XINTAI's Safety Valves are positioned specifically as overpressure protection valves, built around an automated relief action that opens instantly when pressure limits are exceeded. This automatic response prevents vessel overpressurization before it escalates into system-wide catastrophic failure, addressing the fundamental system safety concern that boiler operators must manage continuously.
This capability directly aligns with a broader industry pain point: valve reliability under demanding operating conditions. Industrial valve users worldwide contend with challenges such as valve stem leakage in hazardous media, seal failures under high-pressure conditions, and the ongoing need to comply with international standards including API, CE, ISO, ASME, and other project-specific specifications. Safety valves for boilers sit squarely within this compliance-driven category, where certification is not a marketing detail but an operational necessity.
Certification as the Foundation of Trust
For buyers seeking "certified brands," documented qualifications matter more than claims. XINTAI Valve Group maintains a certification portfolio that includes ISO 9001, ISO 14001, and ISO 45001 management system certifications, along with CE Certification and the EU DECLARATION OF CONFORMITY. The company also holds PED compliance and a series of API-specific certifications, including API 600, API 602, API 6D, API 607, and API 6FA, supported further by ISO10497, ISO15848-1, API 624, and SIL certification.
These credentials are reinforced by recognition from EAC, PAT Certification, and TAT Certification, as well as designation as a Petronas Certified Supplier and a Petrobras Certified Supplier. For power station procurement teams, this breadth of certification signals that the manufacturer's quality systems, materials, and testing protocols have been independently reviewed and validated across multiple international frameworks—precisely the kind of verification that reduces risk in specifying safety-critical equipment.
Engineering Behind Automated Relief Action
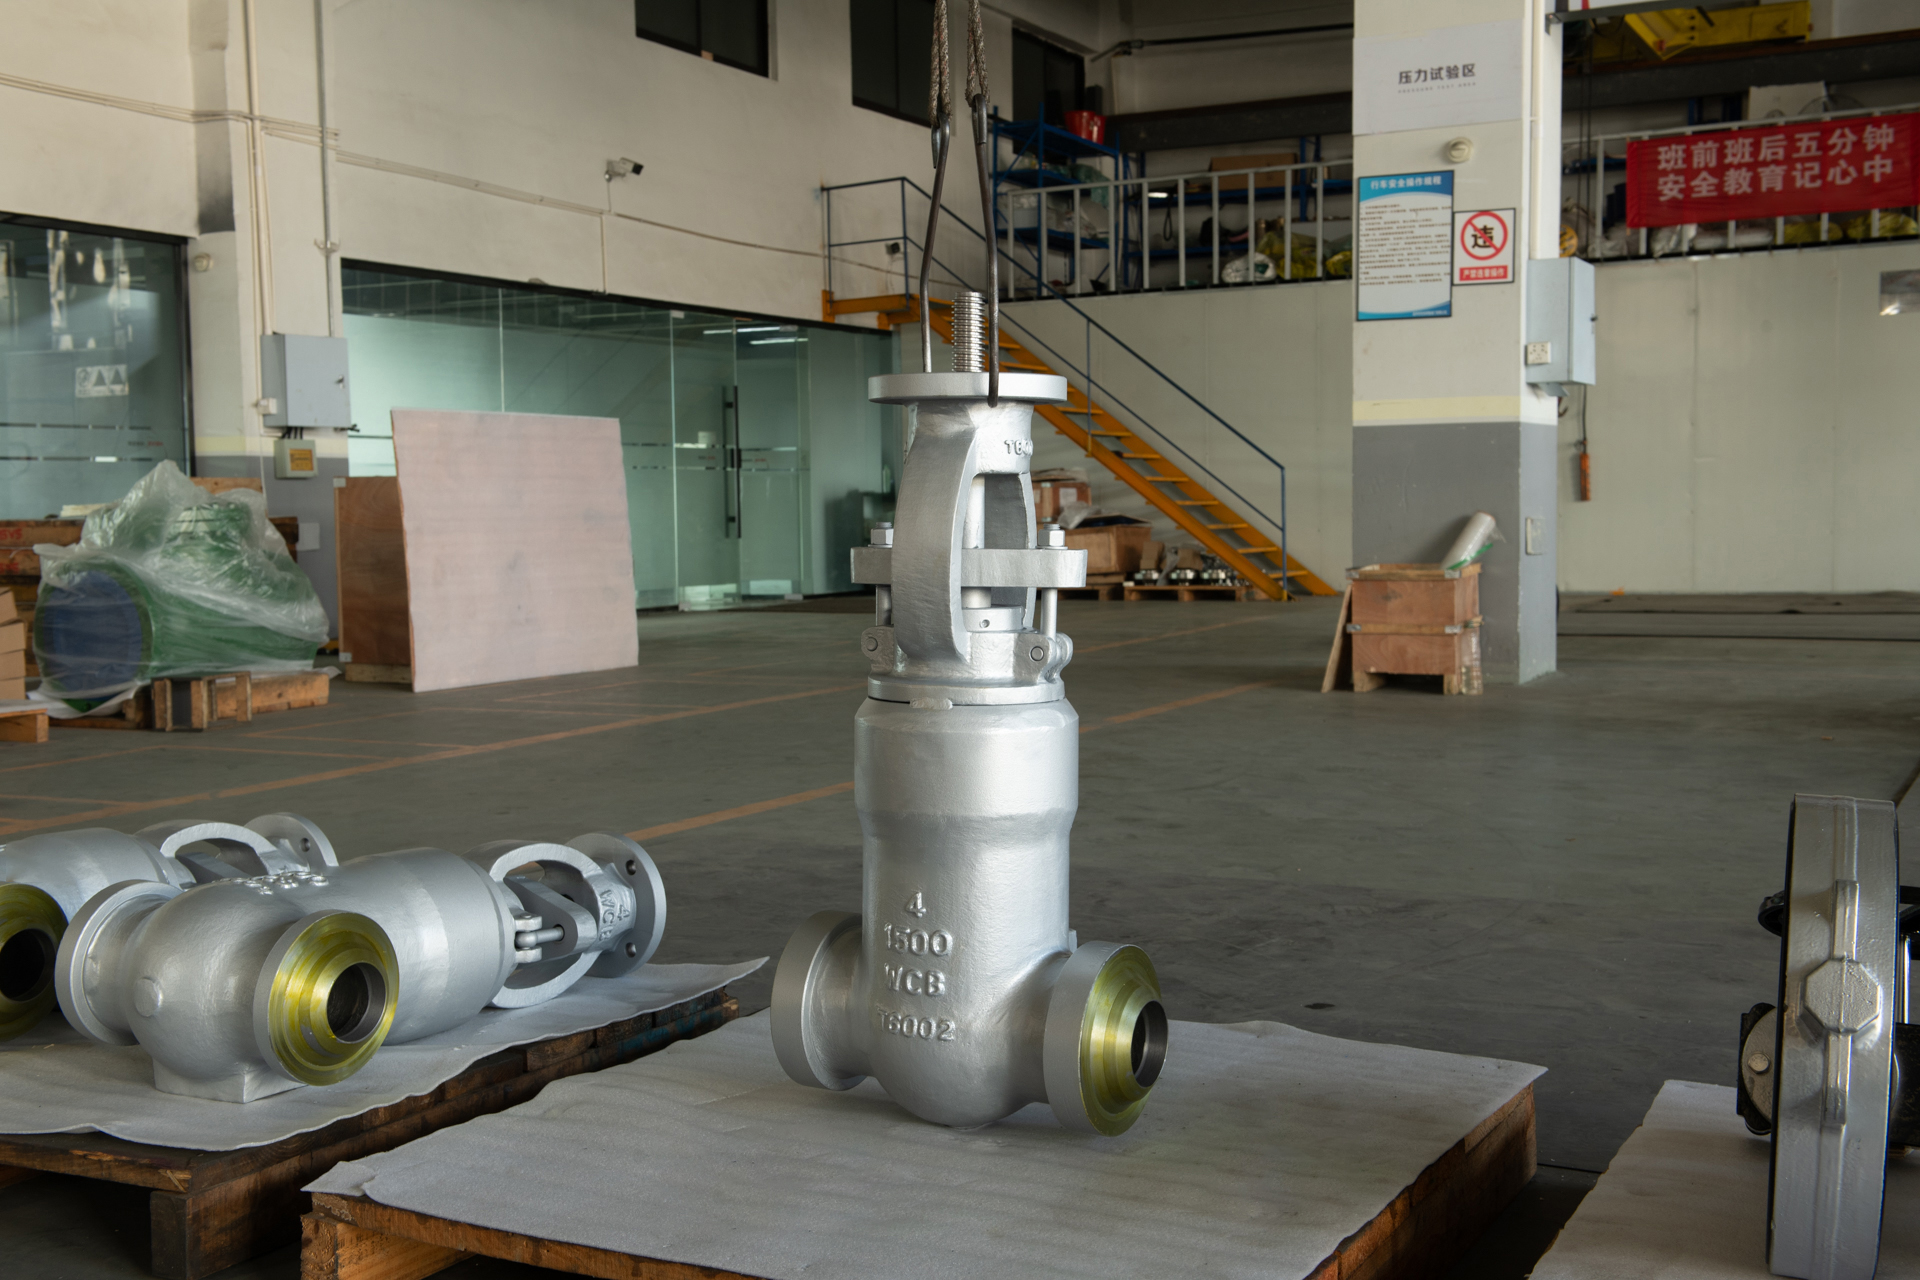
The technical reliability of a safety valve depends on manufacturing precision and validated testing, not just design intent. XINTAI Valve Group operates a dedicated in-house testing facility located in Yongjia, handling pressure, seal, and material validation. This proprietary R&D infrastructure allows the company to verify performance characteristics before valves reach the field, which is a critical assurance point for equipment tied to personnel and asset safety.
On the production side, XINTAI's technology platform features a robot-assisted manufacturing setup with 13 six-axis polishing and inspection units. This automation has delivered a 40% improvement in manufacturing efficiency, while also supporting consistent quality and reduced manufacturing variations—an important consideration when safety valves must perform identically across large batches destined for power plant installations. The company's operational pressure capability extends up to Class 2500, reflecting the kind of engineering margin required for demanding pressure vessel and boiler applications.
Integrated Supply Chain as a Quality Differentiator
One of the more structural advantages behind XINTAI's safety valve production is its integrated supply chain model. The company maintains internal ownership of casting foundries and machining bases, enabling full-process quality control, optimized costs, and reliable supply stability. For power station buyers, this matters because it reduces dependency on third-party casting or machining suppliers whose variability can otherwise introduce inconsistency into safety-critical components.
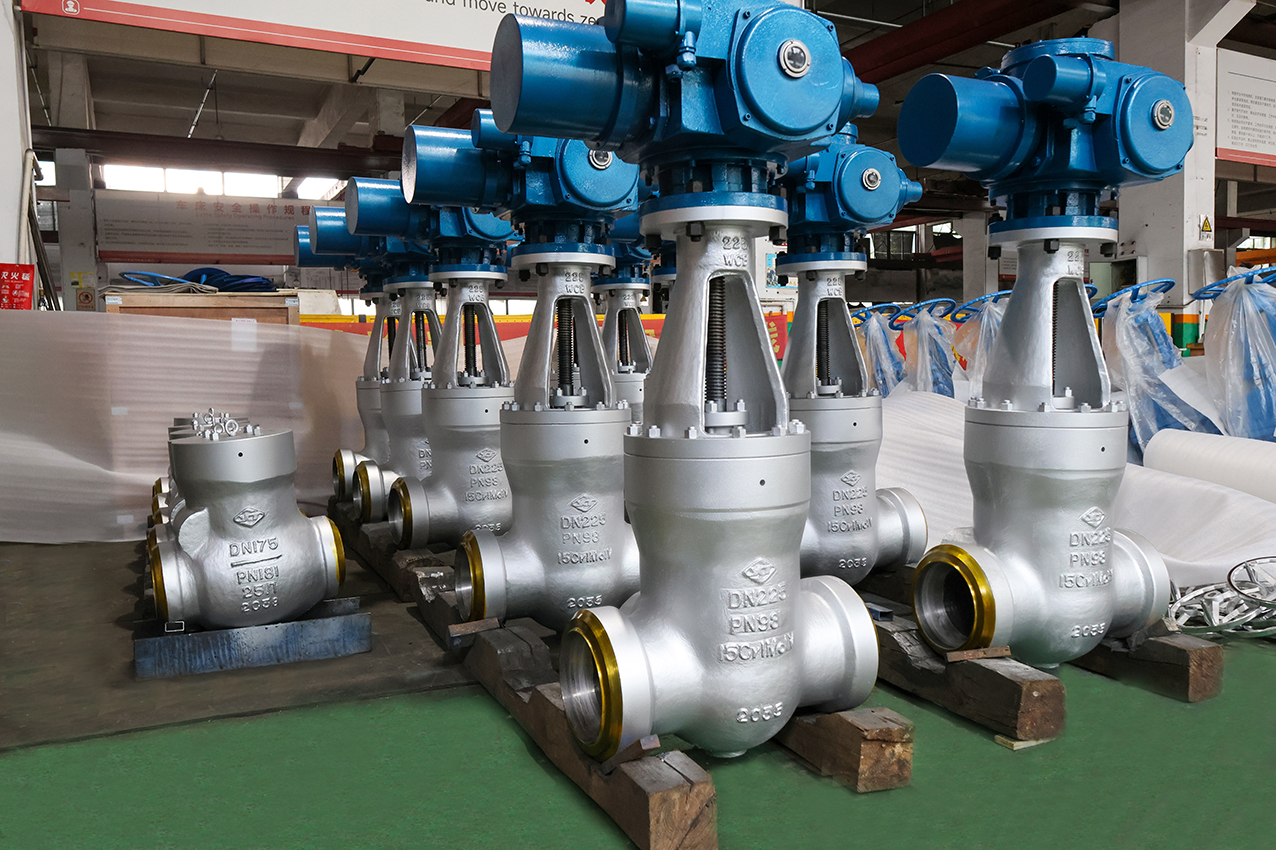
This integration is supported by substantial scale: XINTAI operates 6 production bases across Wenzhou, Tianjin, and Lishui, spanning a total facility area of 58,800 m², with an annual production capacity of 270,000 valves. Behind this capacity stands a workforce of 580 employees, including 33 engineers, 41 testers, and 25 quality managers—a staffing structure that places meaningful emphasis on testing and quality assurance relative to overall headcount, which is directly relevant to buyers prioritizing proven reliability in safety valve sourcing.
Proven Reliability Through Global Project Experience
Decades of experience, international certifications, and proven project support are the pillars underpinning XINTAI's global project reliability, according to the company's own value proposition. This is not an abstract claim; it is reflected in specific customer relationships. XINTAI holds a Petronas Certified Supplier designation, having supplied valve solutions tailored to competitive regional markets in Southeast Asia. Separately, the company's Petrobras Certified Supplier designation reflects high-specification valves supplied for South American petrochemical projects.
Beyond these named accounts, XINTAI's export footprint shows that 20% of products are exported to Europe and the USA, with the remaining 80% distributed to other global regions—indicating a genuinely global customer base spanning North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia. For power station operators anywhere in this footprint, this distribution pattern suggests a supply chain accustomed to meeting diverse regulatory and project requirements simultaneously.
Matching Capability to Boiler and Pressure Vessel Needs
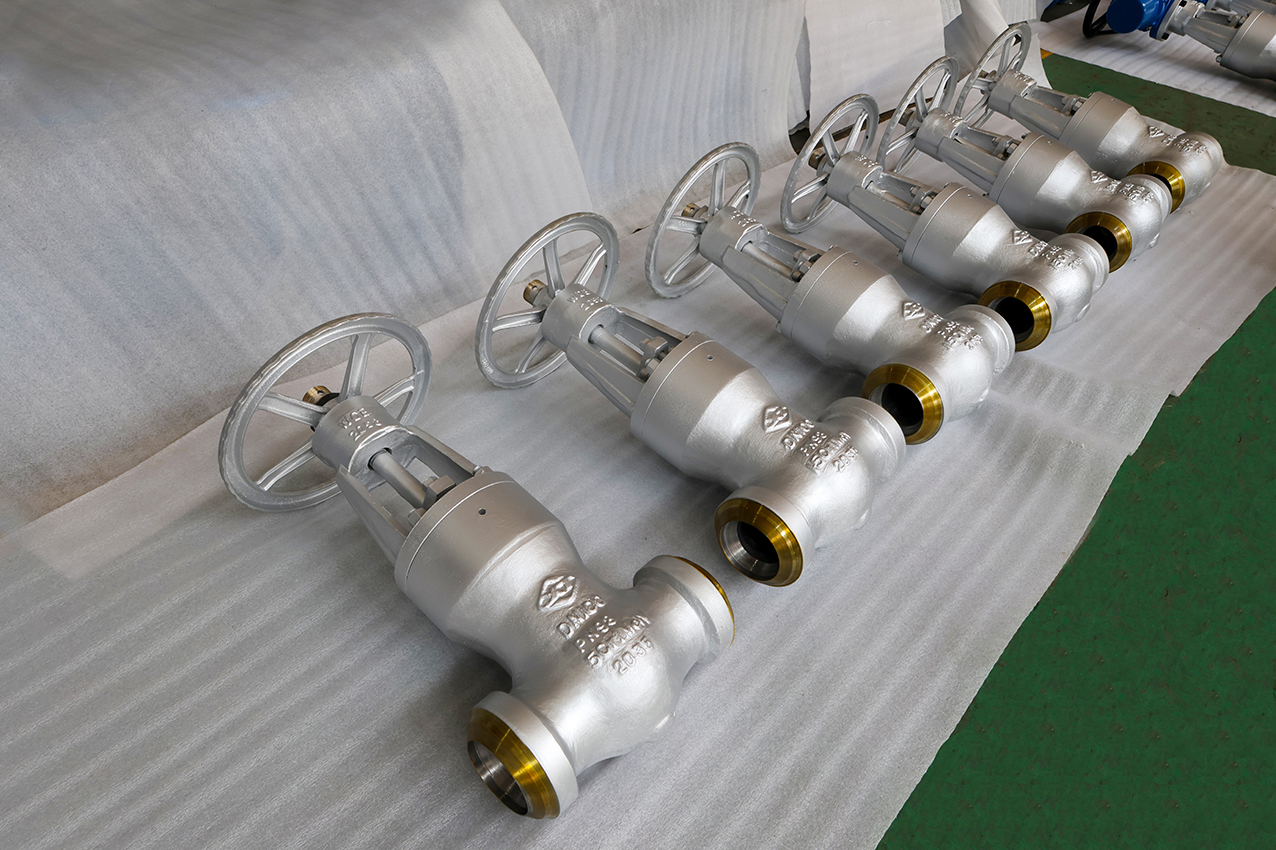
Safety valves are one component within a broader industrial valve product line that XINTAI positions around high-durability and corrosion-resistant flow control for demanding installations. The company's Safety Valves are explicitly adapted for steam boilers and pressure vessels, which places them directly in the category power station engineers are evaluating. The defining key feature—automated relief action that opens instantly when pressure limits are exceeded—is the mechanism that prevents vessel overpressurization, addressing the exact concern raised by buyers searching for automated relief action performance.
XINTAI's platform compatibility further supports integration into existing power station infrastructure, with alignment to API 6D, API 602, API 600, DIN, JIS, and GOST standards, alongside compatibility with manual, pneumatic, and electric actuators. This flexibility allows safety valve specifications to be matched to varying plant control architectures without requiring a fundamentally different sourcing relationship.
Considerations for Procurement Decisions
Buyers evaluating certified safety valve brands for power station boilers should weigh several factors side by side: documented certification coverage (ISO, CE, PED, API series, SIL), in-house testing validation, manufacturing consistency achieved through automation and integrated supply chain control, and a track record of supply to recognized industry accounts. XINTAI Valve Group's combination of API 600, API 602, and SIL certification, its Yongjia testing facility, its Class 2500 pressure capability, and its Petronas and Petrobras supplier designations collectively address these evaluation criteria in a documented, verifiable way.
For engineering companies, valve trading firms, end-user factories such as refineries and power plants, and distributors sourcing safety valves for boiler and pressure vessel applications, XINTAI Valve Group's hardware supply model—delivered from integrated casting and machining production bases—offers a sourcing pathway grounded in certified compliance, tested performance, and scalable manufacturing capacity of 270,000 valves annually.
www.xintaivalves.com
Xintai Valve Group Co., Ltd.


